Dust Monitor Cross Reference: What Actually Replaces a Discontinued Unit
Quick Answer
A dust monitor cross reference means matching output signal, mounting flange, probe length, hazardous area rating, and communication protocol against the original unit, not a similar-sounding model number, before you commit to a discontinued dust monitor replacement.
Your baghouse stack monitor fails on a Tuesday, you call the manufacturer for a replacement sensing head, and the person on the other end tells you the model was discontinued three years ago. This happens in dust monitoring more than in almost any other instrumentation category, because the sensing technology itself has shifted twice in the last two decades while the duct it is bolted to kept running unchanged. A dust monitor cross reference is not about finding a unit with a similar part number stamped on the box. It means matching the things that actually determine whether a replacement works on day one: output signal type, mounting flange and probe length, process connection, hazardous area certification where the stack location genuinely requires it, and the communication protocol feeding your DCS or PLC. Get any one of those wrong and procurement has bought a second problem instead of a fix.
At Techno Control Corp we field this call regularly from cement plants, steel re-rolling mills, and power generation sites across Pakistan and the Gulf: a dust monitor on a baghouse exhaust, a kiln stack, or an emissions compliance point has failed, and the nameplate model is no longer in production. Continuous emissions dust monitor replacement is rarely about availability alone. It is about whether the plant understands what it is actually buying when a dust monitor equivalent from the current catalog shows up with a different sensing principle inside the same-looking housing.
Why Dust Monitors Go Obsolete Faster Than The Equipment They Watch
Two separate forces make an industrial dust monitor obsolete, and they compound each other.
The first is ordinary manufacturer consolidation and product-line churn. The number of independent brands making continuous particulate and bag-leak detection instruments has narrowed over the past two decades as companies have been acquired, merged, or simply retired aging product families in favor of newer electronics platforms. This is not a vague industry rumor; manufacturers publish it directly. Durag, one of the longer-established names in stack-mounted dust and opacity monitoring, has issued formal discontinuation notices for several model generations, including the D-R 300 (discontinued without a direct successor), the D-R 800 (succeeded by the D-R 808), and the first-generation D-R 220 (discontinued at the end of 2017, with service and support listed through December 2027 on Durag's own lifecycle page). That last detail matters for procurement planning: a documented end-of-life horizon is a normal, responsible part of how this market operates, not a sign that something went wrong.
The second force is a genuine shift in sensing technology, and it is the more disruptive one. Early stack-mounted dust monitoring leaned on opacity measurement: a light source and detector across the duct, reading how much the dust cloud attenuates a beam through absorption and scattering, the exact principle EPA's Performance Specification 1 for continuous opacity monitoring systems has governed since the 1970s. Opacity still has a role on high-concentration stacks, but it is a comparatively coarse tool for the low-range readings most baghouse-exit and compliance points need today.
Triboelectric sensing largely took over that lower-range niche from the 1990s onward. A probe extends into the duct, dust particles strike or pass close to its tip, and the resulting charge transfer (a DC "impaction" signal) correlates loosely with particulate loading. It is inexpensive and mechanically simple, which is exactly why so many of the units now reaching end of life across the industry are triboelectric designs from that era. The industrial dust monitor alternative that has displaced a lot of that installed base combines two newer approaches: forward-scatter laser sensing, which measures light scattered off particles at a shallow angle rather than beam attenuation or impaction charge, and induction-based (AC electrostatic) sensing, which reads the alternating charge a dust cloud induces in a probe rather than the DC impaction signal a tribo unit relies on. The EPA's own bag-leak detection technology guidance explicitly recognizes both charge-transfer and light-scattering as separate working principles, which is the clearest non-vendor confirmation that these are genuinely different measurement physics, not marketing labels on the same idea.
An opacity monitor replacement, a triboelectric dust monitor replacement, and a straight like-for-like swap are three different projects wearing the same purchase order.
What Actually Has To Match: The Cross-Reference Checklist
A dust monitor cross reference lives or dies on five items. Skim past any one of them and a dust monitor equivalent that looks right on paper turns into a field problem.
Output Signal And Communication Protocol
Older units frequently offer nothing more than a dry relay contact for a bag-leak alarm plus a basic 4-20mA trend signal, because they predate widespread HART or Modbus adoption on this instrument class. Newer replacements often default to Modbus RTU or Modbus TCP with the analog output treated as an afterthought. If your DCS historian is pulling a 4-20mA trend tag today, a cross reference that ships Modbus-first and buries the analog output behind a configuration menu is not a drop-in part, it is a wiring and tag-mapping project. Confirm the exact signal type, not just "it has an analog output," before the purchase order goes out. Our write-up on 4-20mA, HART, and Foundation Fieldbus covers how to audit what a given analog or digital signal actually carries before you commit to a replacement that changes it.
Mounting Flange And Probe Length
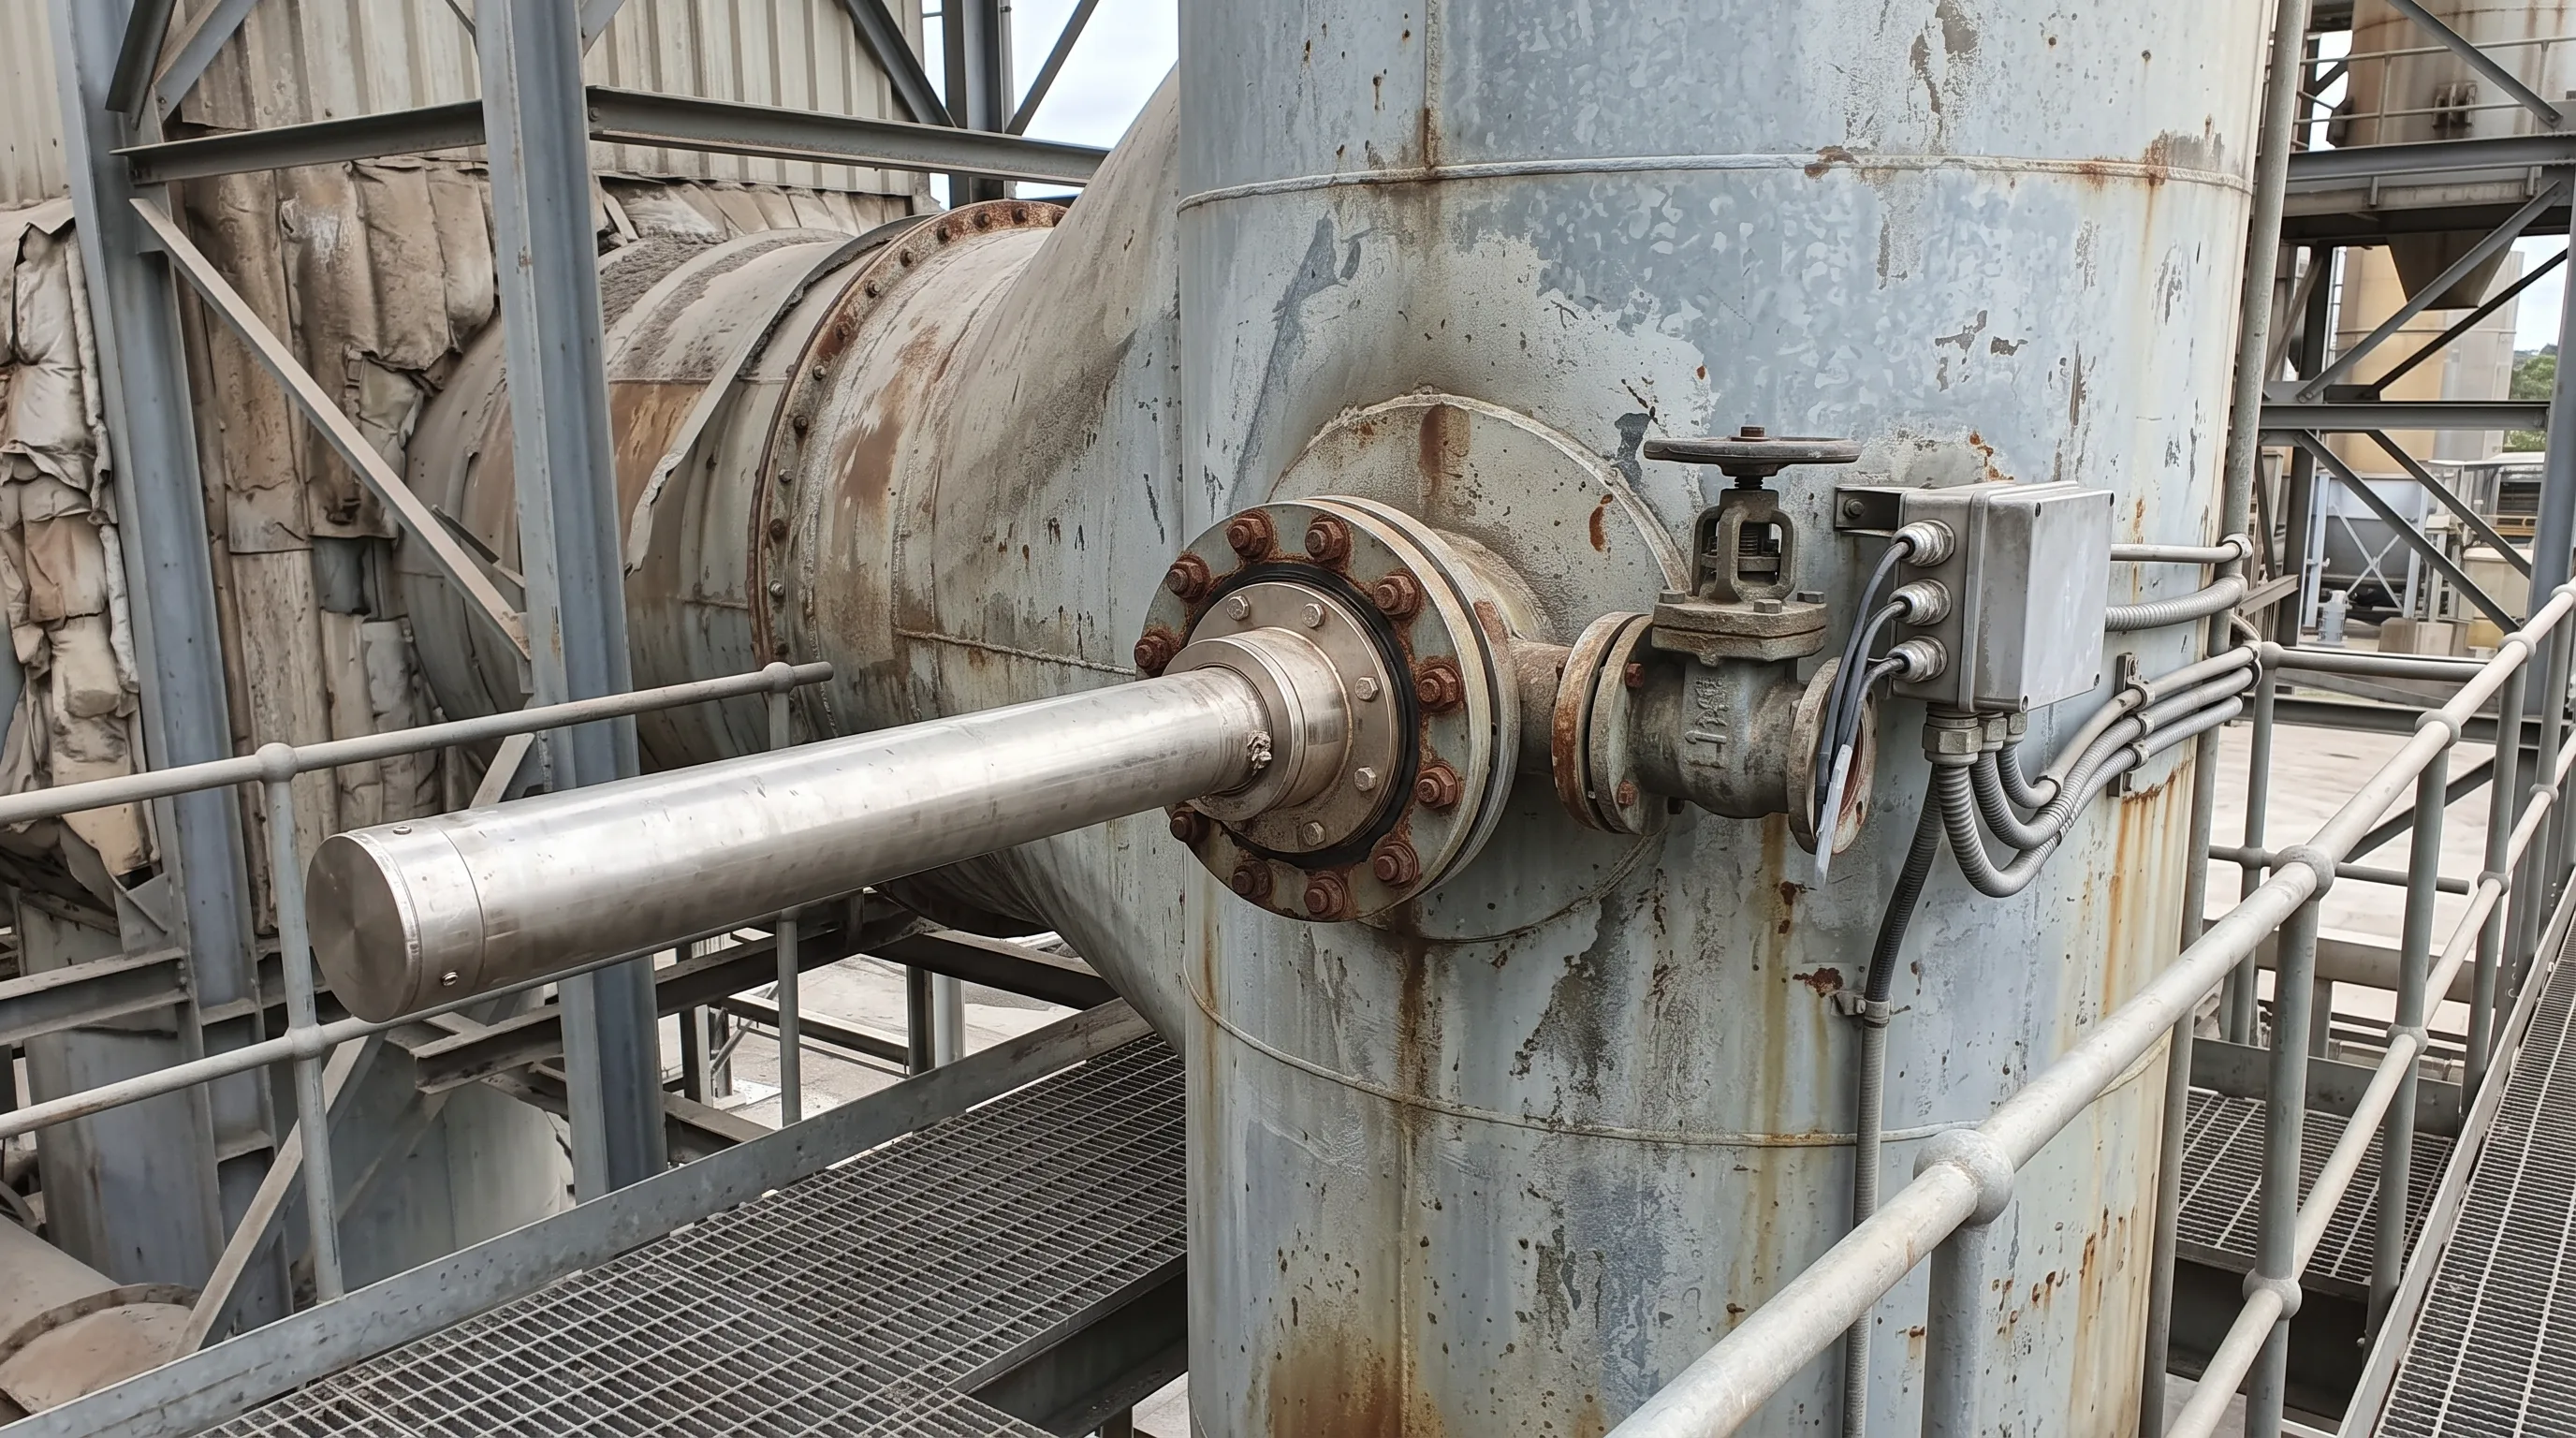
Insertion depth is not cosmetic. A probe that does not reach the representative measurement zone inside the duct, generally away from the duct wall boundary layer and clear of flow disturbances near elbows or dampers, will read low or erratic regardless of how good the sensing electronics are. Flange size (commonly ANSI or DIN pattern), bolt circle, and isolation-ball-valve fittings that let the probe be withdrawn without a full shutdown all need to match the existing cutout, or you are into fabrication work before the instrument even gets powered up.
Process Connection And Sampling Location
Gas temperature at the probe tip, moisture and condensation risk, and corrosive gas exposure (sulfur dioxide and hydrochloric acid are routine concerns on cement kiln and waste-derived fuel lines) determine wetted-material selection and whether purge air is required to keep a window or probe face clean. Equally important: the sampling location itself must stay representative. Reference sampling standards for low-range dust measurement, such as EN 13284-1 in Europe and aligned markets, define sampling-plane and traverse-point requirements precisely because moving a probe to a more convenient but less representative location invalidates any prior correlation between the instrument's raw signal and actual mass concentration.
Hazardous Area Certification Where The Location Actually Requires It
Many baghouse-exit stacks sit downstream of the collector, in clean, cooled flue gas with no combustible dust hazard at all, and need no explosion-protection rating on the monitor itself. Ducts handling combustible organic or metal dust ahead of or inside a collector are a different case entirely. Under IEC classification, that is Zone 20, 21, or 22 depending on how often and how long a combustible dust cloud is present, with dust assigned to Group IIIA, IIIB, or IIIC and equipment marked with protection type ta, tb, or tc under IEC 60079-31. IEC 60079-0, the general requirements standard for explosion-protected equipment construction and marking, moved to its eighth edition in 2026, replacing the 2017 edition, so a certificate referencing the older edition number on paperwork from a previous project is not automatically wrong, but it is worth checking against current ATEX or IECEx documentation rather than assumed. In the United States, the NEC addresses the same hazard under Article 500's Class II, Division 1 or 2, Groups E, F, and G system, or through Article 506's Zone 20/21/22 alternative. Our breakdowns of explosion-proof enclosures versus standard electrical equipment and the Ex d versus Ex db marking distinction both cover how to read a hazardous-area certificate correctly, which is exactly the skill a dust monitor cross reference depends on in any duct where combustible dust is a real possibility.
| Sensing Technology | Measurement Principle | Typical Working Range | Strength | Limitation |
|---|---|---|---|---|
| Opacity | Light beam attenuation across the duct | Moderate to high concentration | Simple, long field history, good on visibly dense plumes | Comparatively coarse at low (sub-50 mg/m3) concentrations |
| Triboelectric (DC impaction) | Charge transfer when dust strikes or passes the probe tip | Low to moderate concentration | Low cost, simple installation, long-standing bag-leak standard | Signal drifts with probe buildup, flow velocity, and particle composition |
| Inductive (AC electrostatic) | Alternating charge induced in the probe by the passing dust cloud | Low concentration, continuous trending | More linear response than DC tribo, better suited to continuous quantitative trending | Still probe-contamination sensitive, newer installed base, fewer long-term field records |
| Forward-scatter laser | Light scattered at a shallow angle off individual particles | Very low concentration, compliance-grade trending | Recognized by EPA guidance as a distinct working principle, strong low-range sensitivity | Optics need purge air and periodic cleaning to avoid drift from window fouling |
Drop-In Cross Reference Versus Technology Upgrade: Two Different Projects
A genuine drop-in cross reference keeps the same sensing principle and output type and simply bolts a current-production unit into the existing flange. Recommissioning is a zero and span check, maybe a short functional alarm test, and the plant moves on.
A technology upgrade is a different animal, even when the new unit physically bolts into the same hole. Moving from opacity to forward scatter, or from DC triboelectric to combined DC and AC induction sensing, changes the underlying measurement physics. The relationship between the instrument's raw output and actual particulate mass concentration in mg/m3 has to be re-established, not assumed to carry over. That re-establishment is a correlation test against a manual isokinetic reference method: EN 13284-1 gravimetric sampling in Europe and aligned markets, or EPA Methods 5, 5I, or 17 in the United States under Performance Specification 11 (40 CFR Part 60, Appendix B). In jurisdictions following the European framework, this correlation runs under the QAL2 procedure defined in EN 14181 together with the dust-specific calibration and validation requirements in EN 13284-2, which applies below 50 mg/m3. In the US framework, ongoing QA after the initial PS-11 correlation runs under Procedure 2 of Appendix F.
A dust monitor cross reference that swaps sensing technology without a fresh isokinetic correlation test is not a calibration. It is a guess wearing a calibration certificate.
Budget for this distinction before the purchase order is signed, not after the new unit is already bolted in and reading numbers nobody can defend to an auditor.
A Real-World Scenario: The Cement Kiln That Traded One Problem For Another
A cement plant running a roughly 2,000 tonne-per-day kiln line had a triboelectric probe monitoring the main baghouse stack, installed new in 2010 for both bag-leak detection and emissions compliance trending. The probe failed outright in 2024. The original manufacturer's local distributor confirmed the model was discontinued, with no direct sensing-head replacement, and recommended a current-production unit from the same brand as the "equivalent."
The replacement physically fit the existing flange and probe length, so the site treated it as a straight swap. It was not. The new unit used forward-scatter sensing, not DC triboelectric. The plant's existing bag-leak alarm setpoint, tuned years earlier to a value that corresponded to roughly 20 mg/m3 on the old triboelectric scale, carried over unchanged into the new instrument's configuration because nobody flagged that the two sensing principles do not share a common raw-signal scale. For weeks the stack trended quietly inside what looked like a normal range on the new sensor while a bag actually degraded, because the inherited setpoint no longer corresponded to a meaningful particulate level on the new device's output curve. The failure surfaced only when a routine stack test under the reference method found particulate loading well above what the "equivalent" monitor had been reporting.
The equipment choice was not the mistake. Treating a technology upgrade as if it were a drop-in cross reference was. A short correlation check against a manual isokinetic reference run at commissioning would have caught the mismatch before it cost the plant a stack-test finding and an unplanned bag change-out.
When Retrofit Beats Full Replacement
A dust monitor retrofit is worth pricing out before a full replacement goes out for quote, because it is often the cheaper path when the manufacturer still supports it. Retrofit means keeping the housing, mounting flange, probe tube, junction box, and often the existing cable run, and replacing only the sensing head or transmitter electronics where the manufacturer genuinely supports that upgrade path for that specific housing family. Durag's own D-R 800 to D-R 808 transition, published as a named successor rather than a dead end, is exactly the kind of documented path that makes a dust monitor retrofit a realistic option rather than wishful thinking.
Retrofit is the right call when three things line up: the manufacturer still offers a sensor-head-only upgrade compatible with the existing housing and probe geometry, the duct access and insertion depth stay unchanged, and any hazardous-area certification on the installation still covers the new internals. That third point catches people out. Explosion-protection certification generally applies to a complete assembly as tested, not to a housing in isolation, so a legacy dust monitor replacement that only swaps internals still needs the paperwork checked, not assumed.
Full replacement wins when the flange standard itself has been discontinued, when the new electronics package needs a different probe length than the existing cutout allows, or when the hazardous-area certification was issued for the original assembly as a whole and does not automatically extend to a modified unit. Compare total installed cost, not list price, before deciding; a cheaper retrofit kit that needs a field engineer to requalify the Ex certification on site can cost more than a certified, pre-tested replacement unit shipped complete.
Procurement Steps To Avoid A Second Mistake
Before ordering a baghouse dust monitor replacement, or committing to any discontinued dust monitor replacement, work through this sequence rather than matching a model number from memory. Treating any particulate monitor replacement as a routine parts order, without walking through these steps, is how the cement kiln scenario above happens a second time:
- Pull the original nameplate data first: exact model, serial number, output type, and any hazardous-area marking stamped on the unit itself, not just what the original purchase order said a decade ago.
- Physically measure probe insertion depth and flange bolt pattern on site. Duct modifications happen over the years, and datasheets drawn up at commissioning do not always reflect what is actually bolted in today.
- Confirm the current hazardous-area classification of that specific duct location rather than inheriting an assumption from the original installation. Dust loading, process changes, and even collector upgrades can change the classification.
- Specify the exact communication protocol and verify it against your current DCS or PLC tag mapping before the order goes out, not after the box arrives.
- Ask the vendor directly whether the proposed unit is a drop-in cross reference or a sensing-technology change. If it is a change, budget for a correlation test against the manual isokinetic reference method and get a qualified stack-testing contractor scheduled before commissioning, not scrambled together afterward.
- Get a written spares and support commitment from whichever manufacturer you choose this time. A stated end-of-life horizon, the same kind Durag now publishes for its own retired models, turns the next obsolescence event into a planned replacement cycle instead of another emergency call.
Stack-mounted dust and opacity monitors sit in the same instrumentation family as the flow, pressure, and level devices that keep a process under control, and the same discipline applies: match the physics, not just the mounting hole, before trusting the number on the display. Our piece on flowmeter troubleshooting walks through a parallel case where a technically "equivalent" replacement instrument produced readings nobody should have trusted without requalification. If your stack dust monitor upgrade also touches how the device talks to your control platform, that is squarely industrial automation territory, and obsolescence planning, including any emission monitoring system replacement, belongs in the same asset-management conversation as the rest of your electrical maintenance and reliability program rather than being handled as a one-off emergency purchase.
If you are staring at a discontinued dust monitor replacement decision and a stack test deadline, Techno Control Corp's instrumentation and control team can run the cross reference properly: confirming output, mounting, hazardous-area certification, and protocol compatibility before you commit to a unit, and coordinating the correlation testing if the right answer turns out to be a dust monitoring system upgrade rather than a straight swap. Our product catalog includes certified replacement instrumentation sourced through verified manufacturer channels for exactly this kind of legacy dust monitor replacement or particulate monitor replacement project.
Frequently Asked Questions
What can replace a discontinued industrial dust monitor?
Either a drop-in cross reference, a current-production unit from the same or another manufacturer that matches the original output signal, mounting flange, probe length, and hazardous-area rating, or a technology upgrade to forward-scatter or inductive sensing if no matching sensing principle is still in production. The right answer depends on what is actually discontinued: the model, or the entire sensing principle it used.
How do I find a cross reference for an obsolete dust monitor?
Start with the original nameplate data (model, serial, output type, certification marking), then check whether the original manufacturer has published a discontinued-model notice naming a successor, since several manufacturers, including Durag, document exactly this transition. If no direct successor exists, a qualified instrumentation supplier can run a formal cross reference against output signal, mounting geometry, process connection, and protocol rather than matching on appearance alone.
Can an old triboelectric dust monitor be retrofitted instead of replaced?
Sometimes. Retrofit works when the manufacturer still offers a sensor-head-only upgrade compatible with the existing housing and probe length, and when any hazardous-area certification on the installation still covers the upgraded internals. It does not work when the flange standard is discontinued, the new electronics need a different probe length, or the explosion-protection certificate was issued for the original assembly as a whole.
What should I check before replacing a particulate monitor?
Before you replace obsolete dust monitor hardware, verify the output signal and communication protocol against your DCS or PLC tag mapping. Confirm the mounting flange and probe insertion depth physically on site, and check the current hazardous-area classification of that duct location. Then establish whether you are doing a drop-in cross reference or a sensing-technology change; the second needs a fresh correlation test against the manual isokinetic reference method before you trust the readings.
Related products
Components from our catalogue relevant to this article — request a quote for availability, lead time and pricing.
/BAT53 Series Explosion Proof Led Flood Light 70W-1000W For Hazardous Areas.webp "ATEX BAT53 Series ATEX - Explosion Proof LED Flood Light 70W-1000W | Explosion-proof LED floodlight, 70W-1000W")
BAT53 Series ATEX - Explosion Proof LED Flood Light 70W-1000W
Explosion-proof LED floodlight, 70W-1000W
/BAT85 Series Explosion Proof Floodlights , ATEX Led Flood Light.webp "ATEX BAT85 Series ATEX - Explosion Proof Floodlight, LED Flood Light | ATEX-certified explosion-proof LED floodlight")
BAT85 Series ATEX - Explosion Proof Floodlight, LED Flood Light
ATEX-certified explosion-proof LED floodlight
/BnT81 Series Aluminium ATEX Floodlights , Hazardous Location ights with 400W~1000W.webp "ATEX BnT81 Series ATEX - Aluminium Floodlight, Hazardous Location Lighting 400W-1000W | Aluminium ATEX floodlight, 400W-1000W")
BnT81 Series ATEX - Aluminium Floodlight, Hazardous Location Lighting 400W-1000W
Aluminium ATEX floodlight, 400W-1000W
/HRD91-LED Series Explosion Proof LED Lighting 30W 50W 70W 100W For Hazardous Areas.webp "ATEX HRD91-LED Series ATEX - Explosion Proof LED Lighting 30W-100W | Explosion-proof LED light, 30W/50W/70W/100W")
HRD91-LED Series ATEX - Explosion Proof LED Lighting 30W-100W
Explosion-proof LED light, 30W/50W/70W/100W